Application requirements
I/O density, cycle time, motion or process requirements, field distances and maintenance needs are assessed together. This defines the requirements of the working system, not just individual products.
This machine automation application uses HMI, PLC and field signals to address field control, reliable communication and maintainable commissioning.
I/O density, cycle time, motion or process requirements, field distances and maintenance needs are assessed together. This defines the requirements of the working system, not just individual products.
The proposed architecture combines HMI, PLC and field signals with the machine’s existing control infrastructure and communication protocols. Final product and module selection depends on site requirements.
ProControl can adapt the solution to local project requirements in Türkiye, from site assessment, I/O planning and protocol selection to panel layout, commissioning and after-sales support.
The technical workflow and visual information from the manufacturer are presented below.
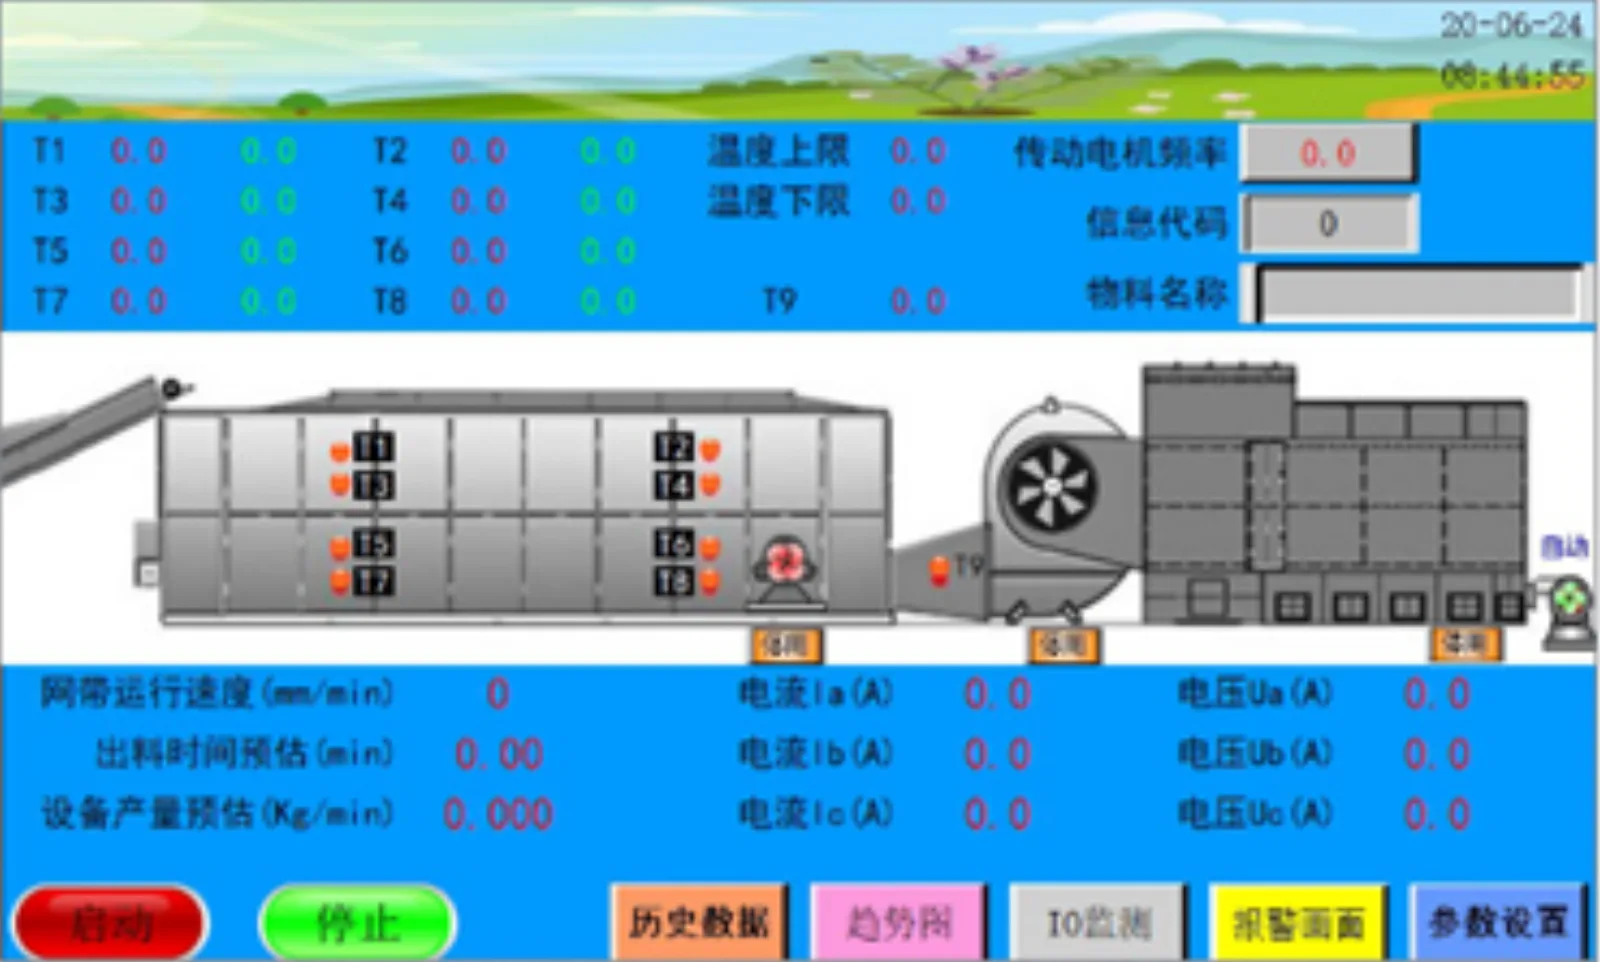
Continuous mesh belt drying machinery requires highly efficient thermal utilization and strict clean-air path segregation to prevent combustion contamination. The process involves routing raw material through an “S”-shaped multi-layer conveyor matrix while managing upward thermal air pressure. To optimize fuel costs using biomass particle combustion exchangers, the automation infrastructure must handle multi-node RS-485 Modbus telemetry, calculate real-time motor RPM speed conversions, and execute automatic threshold fan switching to eliminate uneven dehydration and minimize thermal waste on the factory floor.
| Hardware Category | Implemented Model | Specific Role within the Architecture |
|---|---|---|
| Logic Control Layer | Samkoon FAT-16MT PLC | Primary controller executing Modbus polling loop and computing real-time mathematical estimation algorithms. |
| I/O Expansion Layer | Samkoon S-E8X8T Module | Expands localized discrete inputs/outputs for multi-stage fan relays and safety interlocks. |
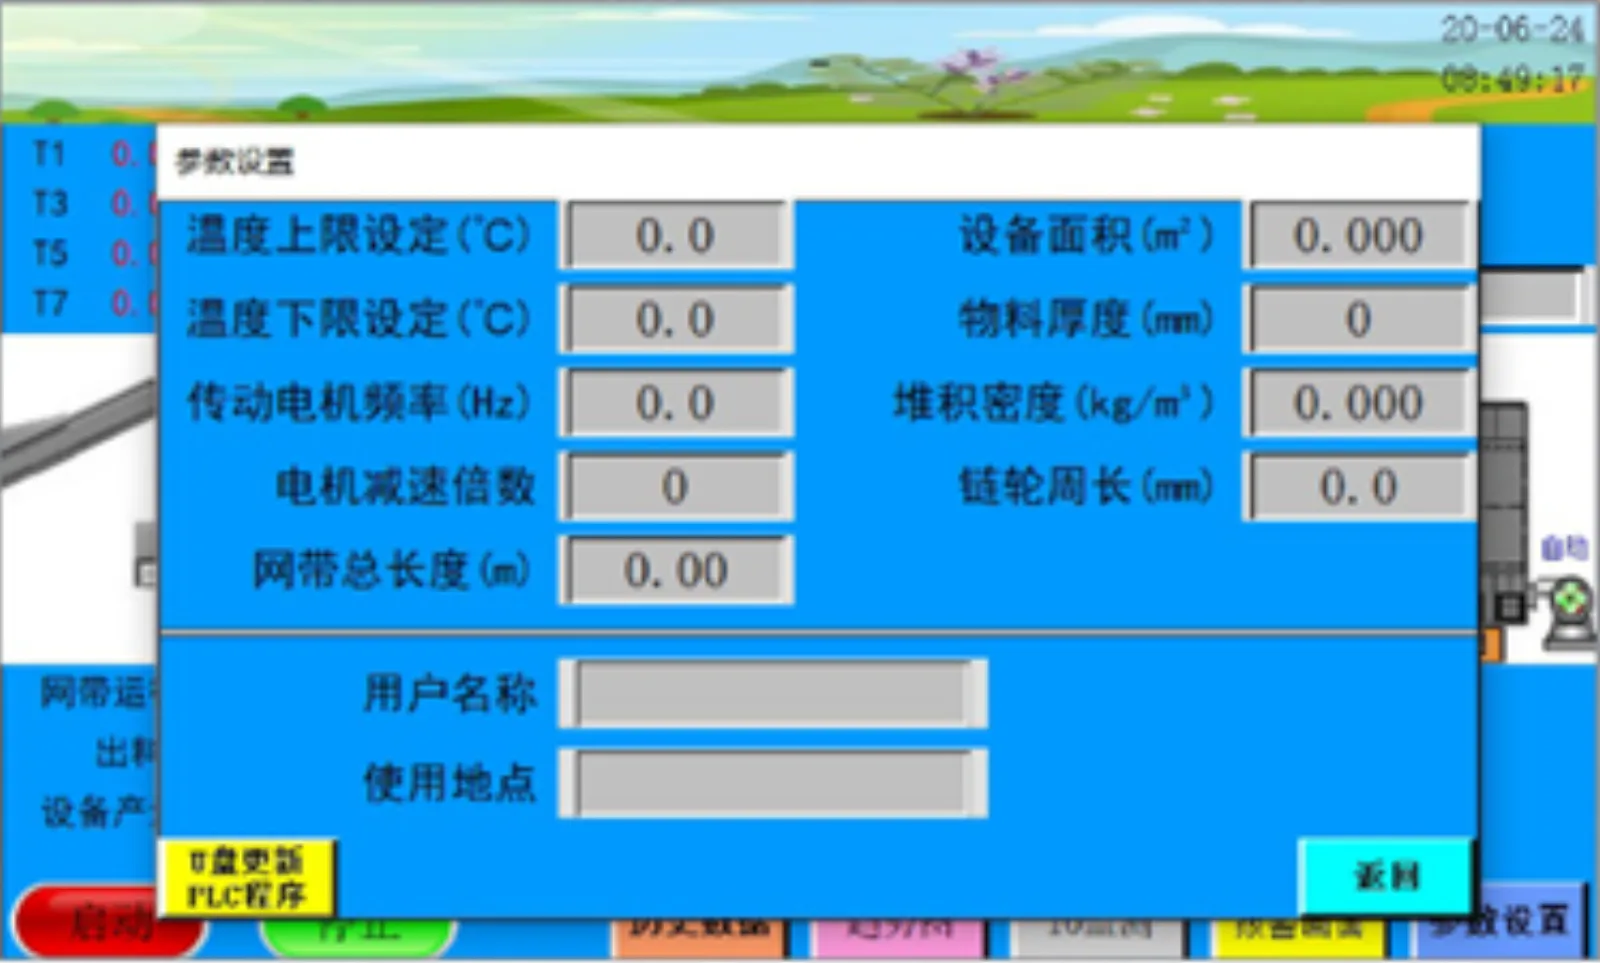
| Operator Interface Layer | Samkoon SK-070QE HMI | Formulates the visualization terminal over a dedicated non-OS micro-kernel. Manages multi-point sensor registers, velocity tracking, and over-six-month telemetry logging. |
| Network & Inverter Layer | Modbus-RTU over RS-485 | Directly interfaces with variable frequency drives (VFD) via digital serial commands to regulate conveyor motor speed dynamically. |
1. Mesh Belt Running Speed (m/min):
Mesh Belt Speed = (Motor Speed / Deceleration Ratio) × 558.8 mm
2. Discharge Time Estimation (min):
Discharge Time = Total Mesh Belt Length / Mesh Belt Running Speed
3. Material Output Estimation (kg/min):
Output = (Equipment Area × Material Thickness × Stacking Density) / Discharge Time