Application requirements
I/O density, cycle time, motion or process requirements, field distances and maintenance needs are assessed together. This defines the requirements of the working system, not just individual products.
This machine automation application uses HMI, PLC and field signals to address field control, reliable communication and maintainable commissioning.
I/O density, cycle time, motion or process requirements, field distances and maintenance needs are assessed together. This defines the requirements of the working system, not just individual products.
The proposed architecture combines HMI, PLC and field signals with the machine’s existing control infrastructure and communication protocols. Final product and module selection depends on site requirements.
ProControl can adapt the solution to local project requirements in Türkiye, from site assessment, I/O planning and protocol selection to panel layout, commissioning and after-sales support.
The technical workflow and visual information from the manufacturer are presented below.
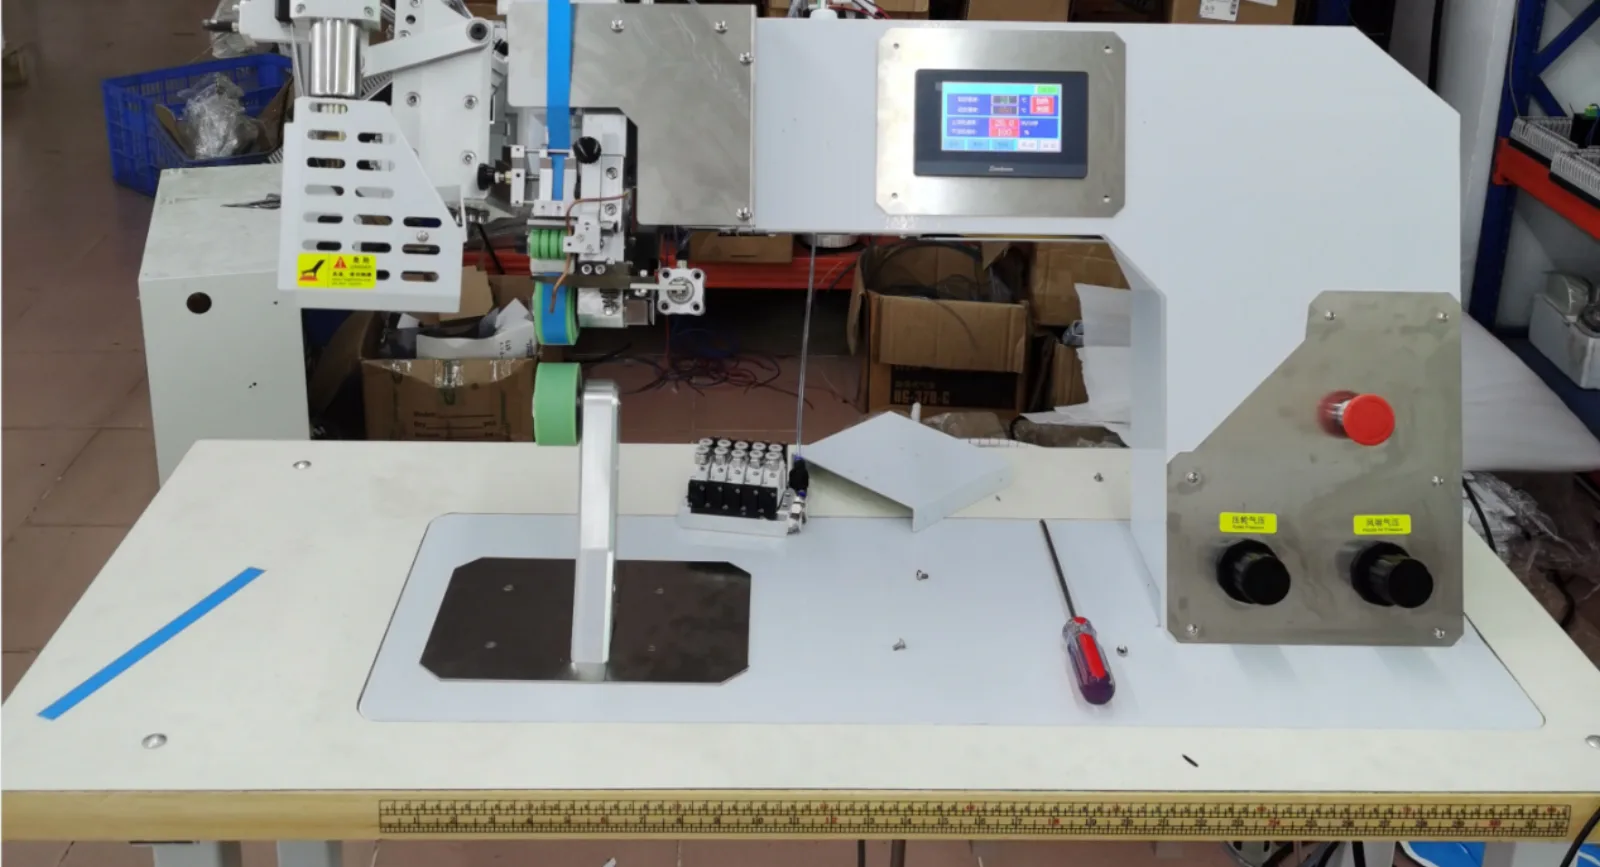
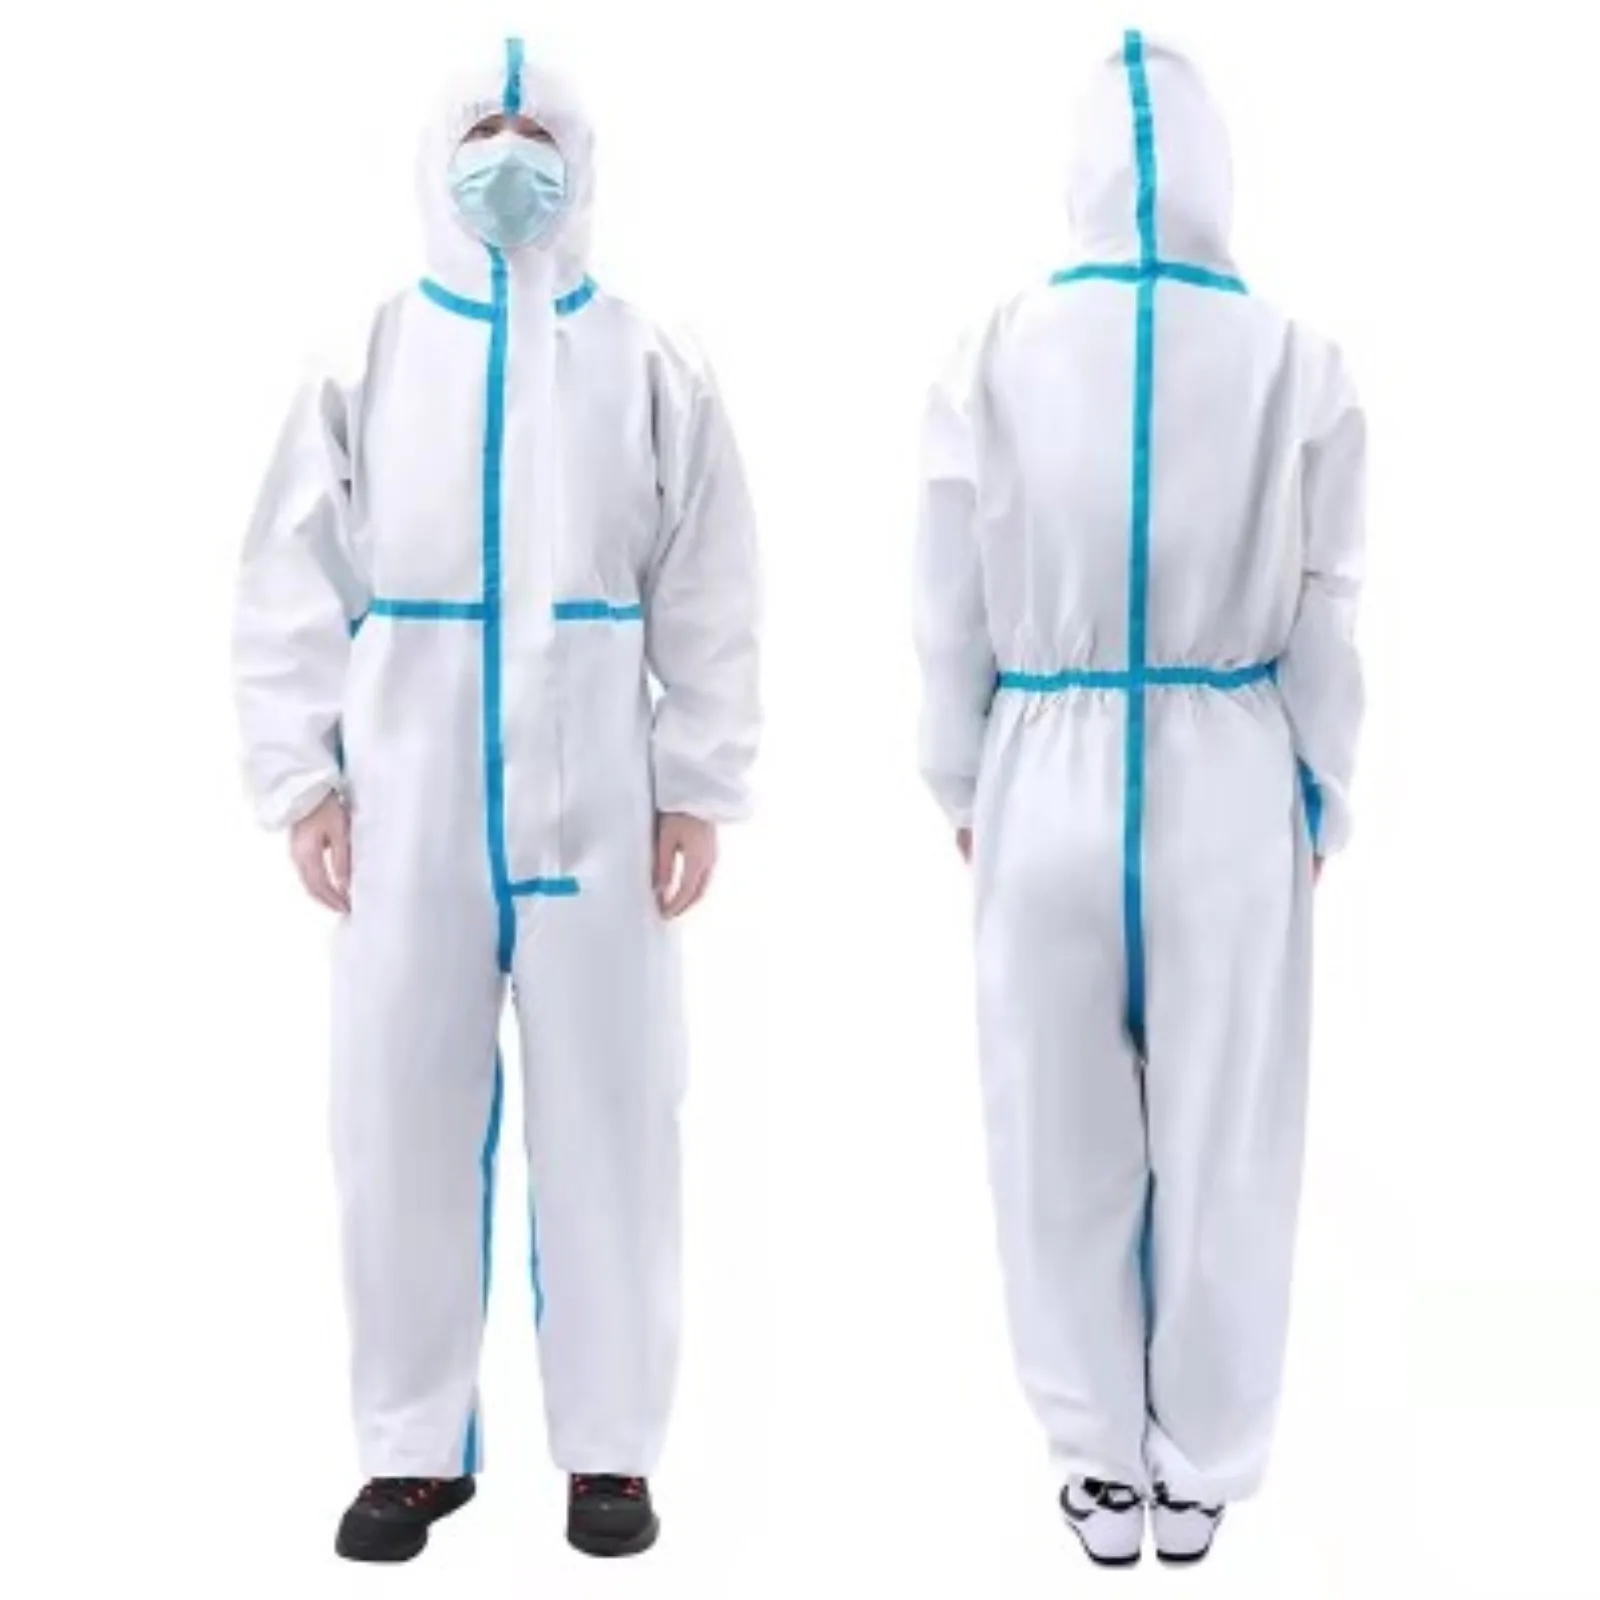
Medical protective clothing manufacturing dictates strict seam-sealing constraints to safeguard personnel against biological and liquid infiltration. The critical process relies on a heavy-duty glue pressing machine (seaming machine) that applies heat-sealing adhesive tape across vulnerable fabric seams. To achieve pristine sealing continuity without scorching the delicate protective material or introducing structural wrinkles, the control automation must execute highly synchronized multi-axis motion, manage responsive pneumatic pressure tracking, and deliver sub-degree thermal stability over intense, continuous production shifts.
| Hardware | Model | Specific Role within the Architecture |
|---|---|---|
| Logic Control Layer | Samkoon FAT-16MT PLC | Primary logic unit running fast cycle times to coordinate pulse trains, analog telemetry, and safety loops. |
| I/O Expansion Layer | Samkoon S-E8X8R + S-E4TC | Expands discrete relays and integrates a high-precision thermocouple tracking interface for real-time thermal loops. |
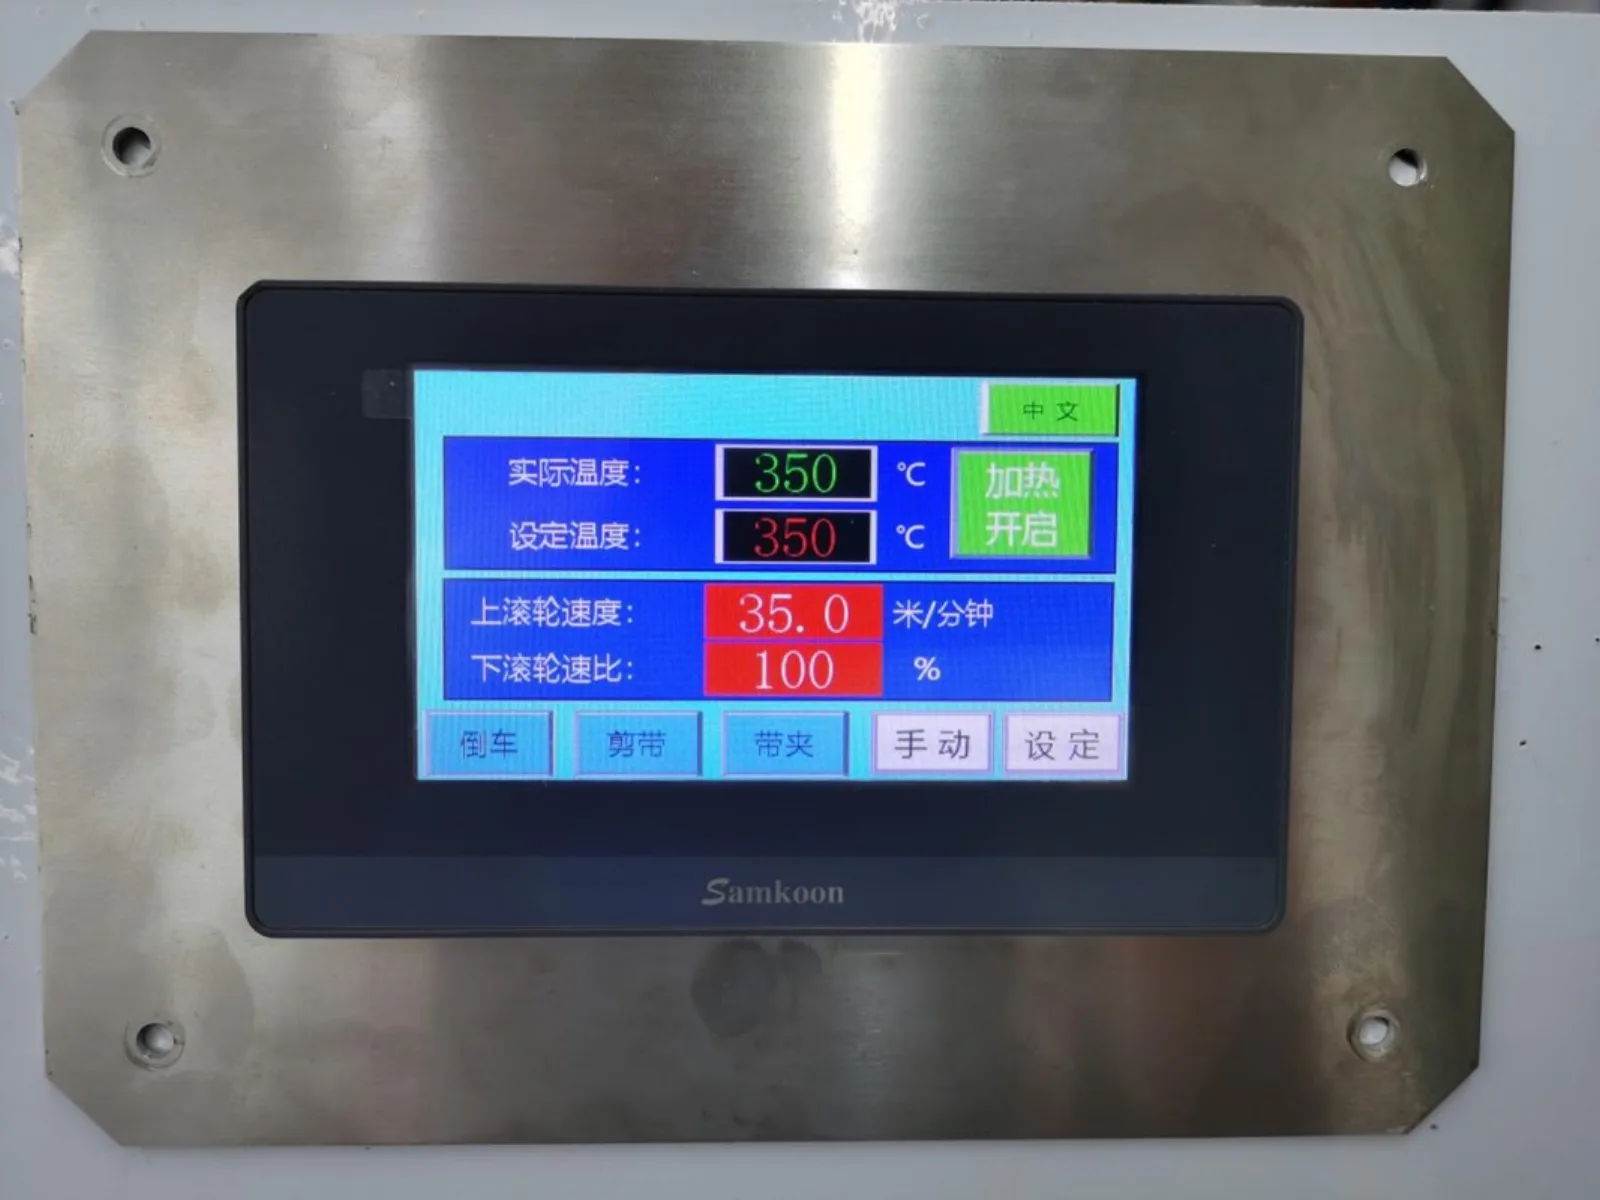
| Operator Interface Layer | Samkoon SK-043QT HMI | 4.3-inch space-saving terminal powered by an industrial Cortex-A7 core. Manages speed ratio calculation, temperature targets tuning, and error warning registers. |
| Motion Execution Layer | Dedicated Stepper Systems | Three independent stepper pulse outputs synchronized to run continuous tape feeding and rollers profiling. |
Actual firmware interfaces and field application layout. The screen capture displays real-time hot air telemetry (350°C actual vs 350°C target), active roller velocity metrics (35.0 m/min), and dedicated sub-menus for automated cutting settings, safety parameters calibration, and I/O status diagnostic registers.